
In the exacting world of precision engineering and manufacturing, accuracy is not just a goal. It is the absolute standard. Whether you are producing complex aerospace components or high-volume automotive parts, ensuring that every feature aligns perfectly with its design intent is critical. This is where Geometric Dimensioning and Tolerancing (GD&T) comes into play. Among the various symbols and controls used in GD&T to define engineering tolerances, “runout” is one of the most common yet frequently misunderstood concepts.
Specifically, the distinction between circular runout (often just called “runout”) and total runout can cause significant confusion on the shop floor and in the design office. Both controls measure the deviation of a rotating part relative to a datum axis, but they do so in fundamentally different ways with vastly different implications for manufacturing costs. Understanding this difference is essential for designers to specify the correct tolerance and for manufacturers to ensure efficient, cost-effective production.
At Castech, we specialise in Precision CNC Machining, where adhering to strict GD&T standards is part of our daily routine. We see the impact of these tolerances on production times and costs every day. In this article, we break down the definitions, symbols, and practical applications of both runout and total runout to help you understand which is right for your project.
The Quick Answer
The primary difference lies in the scope of the control. Circular Runout (indicated by a single arrow) is a 2D control. It checks individual cross sections of a part independently. It ensures that a specific slice of the part is round and centred on the axis, but it does not check the entire surface at once. Total Runout (indicated by a double arrow) is a 3D control. It checks the entire surface simultaneously. It ensures that the whole feature is round, centred, straight, and cylindrical. Consequently, Total Runout is a much stricter tolerance that is harder and more expensive to manufacture than Circular Runout.

What Is Runout in GD&T?
In simple terms, runout measures how much a feature “wobbles” or deviates from a perfect rotation around a central datum axis. Imagine a shaft spinning on a lathe. If you were to hold a marker pen against the surface as it spins, a perfect part would result in a consistent line. A part with runout would push the marker in and out as it turns, creating an uneven line.
Runout is known as a composite tolerance. This means it does not just control one aspect of the geometry. Instead, it simultaneously controls the form, orientation, and sometimes the location of a feature relative to a datum axis.
However, the extent of this control depends entirely on whether you are applying the single arrow of circular runout or the double arrow of total runout.
Circular Runout: The 2D Control
Circular runout is the standard, most commonly used form of runout control. It is often referred to simply as “runout” and is represented by a single arrow (↗) in the feature control frame on an engineering drawing.
How It Works
Circular runout is strictly a two-dimensional (2D) check. It measures the deviation of a circular cross-section at a single point along the axis.
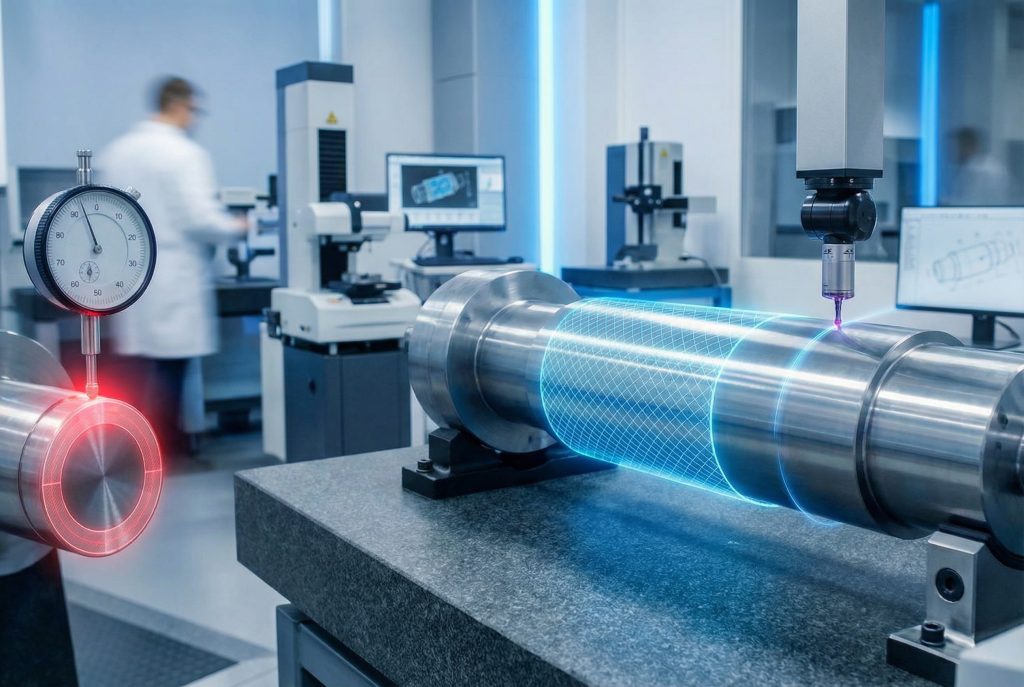
When inspecting for circular runout, a dial indicator is placed at a specific location on the part’s surface. The part is then rotated 360 degrees. The total movement of the dial indicator needle (known as Total Indicator Reading or TIR) represents the runout for that specific cross-section.
Crucially, if you move the dial indicator to a different spot on the shaft, you reset the indicator and start again. The measurement at point A is completely independent of the measurement at point B.
What It Controls
Circular runout effectively controls two geometric characteristics for each slice of the part:
Circularity (Roundness): Is this specific cross-section perfectly round?
Coaxiality (Concentricity): Is the centre of this specific cross-section perfectly aligned with the datum axis?
What It Does Not Control
Because each cross-section is measured independently, circular runout does not control the form of the surface along its length (the profile). For example, a shaft could be tapered like a cone, or bowed like a banana. As long as each slice of that cone or banana is round and centred on the axis of rotation, it would pass a circular runout inspection.
When to Use It
Circular runout is generally cheaper and easier to manufacture and inspect. It is ideal for parts where the primary concern is that the feature rotates smoothly without wobble at specific points. Common applications include:
Shoulders on a shaft where a gear sits.
O-ring grooves where the seal only happens at one specific line of contact.
Short cylindrical features where taper is not a functional concern.

Total Runout: The 3D Control
Total runout is the more rigorous, all-encompassing version of the tolerance. It is represented by a double arrow (↗↗) symbol, which often has a small connecting line at the bottom of the arrows.
How It Works
Total runout is a three-dimensional (3D) check. Unlike circular runout, which checks individual slices one by one, total runout controls the entire specified surface simultaneously.
To measure this, the inspection method changes. The dial indicator is not held at one fixed point. Instead, as the part rotates 360 degrees, the indicator is moved along the full length of the feature (for a cylinder) or across the full face (for a flat surface).
The highest and lowest points recorded across the entire swept surface must fall within the specified tolerance zone. The indicator is never reset during this process.
What It Controls
Total runout is a very powerful control because it limits cumulative errors. It controls all surface variations at the same time. Specifically, it controls:
Circularity (Roundness)
Coaxiality (Concentricity)
Straightness: The surface cannot be bowed or bent.
Cylindricity: The surface must be a true cylinder.
Taper: The diameter cannot change along the length (no cones allowed).
Angularity/Perpendicularity: When applied to a flat surface perpendicular to the axis.
When to Use It
Because it is so strict, total runout is more expensive to achieve. It requires tighter manufacturing controls and more time-consuming inspection. It should be reserved for critical features where the entire surface interacts with another part. Examples include:
Large bearing journals where the entire surface contact is vital for load distribution.
Hydraulic pistons must seal perfectly along their entire length to prevent leakage.
High-speed rotating shafts, where any imbalance or vibration along the length could cause catastrophic failure.
For high precision components used in sectors like polyurethane mouldings or aerospace, total runout ensures that the mould or part fits perfectly into a larger assembly without interference.

The Tolerance Zones Explained
To visualise this, engineers talk about “tolerance zones.”
Circular Runout Zone: Imagine two concentric circles. The line of the part’s surface must fit between these two circles. However, the circles can get bigger or smaller as you move down the shaft (allowing for a taper).
Total Runout Zone: Imagine two concentric cylinders (pipes). The entire surface of the part must fit inside the gap between the inner pipe and the outer pipe. This zone is rigid. It does not allow the part to expand or contract along its length. This is why total runout automatically controls taper and straightness.
Why Is the Distinction Important for Cost?
Choosing between circular and total runout is a balancing act between functionality and cost. In manufacturing, tightening a tolerance always increases the price.
If a design engineer specifies total runout on a feature that only requires circular runout, they are likely increasing the part’s cost unnecessarily. The manufacturer may need to perform additional machining passes, utilise higher-precision lathes, or conduct slow, complex inspections to ensure the entire surface is perfectly cylindrical. In reality, a slight taper might have been perfectly acceptable for the part’s function.
Conversely, if a designer specifies circular runout for a critical bearing surface that actually needs to be perfectly flat and straight, the part might pass the easier inspection but fail in the real world. It could cause vibration, uneven wear, or fluid leaks.
Measuring Runout in Quality Control
Verifying these tolerances requires precise metrology equipment. At Castech, our Quality Assurance processes utilise advanced Coordinate Measuring Machines (CMMs) and traditional dial indicators to ensure every component meets its GD&T specifications.
For Circular Runout Inspection: The part is typically mounted on a V-block or between centres to allow rotation. A dial indicator is positioned against the surface. The part is rotated, and the variation is recorded. The probe is then moved to a new spot, reset to zero, and the process is repeated.
For Total Runout Inspection: The setup is similar, but the process is continuous. The dial indicator must travel along the datum axis while the part rotates, effectively spiralling over the entire surface to find the maximum deviation. Any spike, dip, or taper anywhere on that surface counts against the tolerance.

Conclusion
While the symbols look similar on a blueprint, the single arrow of circular runout and the double arrow of total runout serve very different purposes. Circular runout is your “spot check” for roundness and concentricity, perfect for simple positioning and sealing. Total runout is your “full scan” for complete surface geometry, essential for high performance interfaces and dynamic balance.
Understanding these symbols allows for better communication between design engineers and machinists, ensuring that parts are not just made to print, but are made efficiently and function perfectly.